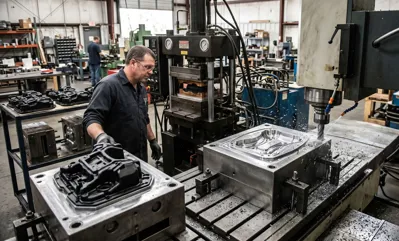
plastik kaucuk kalıp emin pul konya
KAUÇUK PLASTİK KALIP
Home Capacity & Services Industrial Blog Contact
Request RFQ
© 2026 Kaucuk Plastik Kalıp A.Ş.
ISO 9001:2015 Certificated
Mühendislik Günlüğü

Industrial Knowledge Base

Filtered Tag: liquid silicone injection
Clear Filter [X]
Mold gas release and burn prevention.
September 26 178 Views

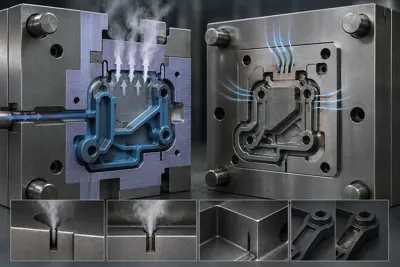
Mold gas release and burn prevention.

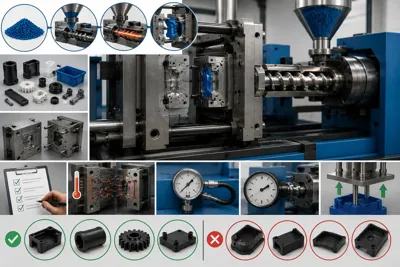
In plastic injection molds, gas venting (ventilation) refers to the design of microchannels that allow the expulsion of ambient air and volatile gases released from the polymer melt during injection. In cases of insufficient gas venting, the trapped gas compresses adiabatically, overheats (>600°C), and creates dieseling/burn marks, leading to black burn marks on the part, short shots, and corrosion of the mold steel. Ventilation depths designed according to polymer viscosity (0.010 mm - 0.040 mm) and sintered porous steel (Porcerax II) inserts reduce the risk of burn marks to zero, increasing cycle speed and weld line strength.
Plastic gear molds
September 26 190 Views

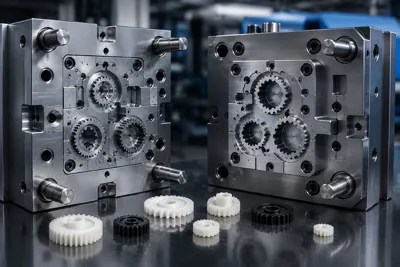
Plastic gear molds

The design of precision plastic gear molds encompasses the production of quiet, high-torque gears used in automotive actuators, medical infusion pumps, and household appliance gearboxes, conforming to AGMA (American Gear Manufacturers Association) and DIN 3967 quality classes (AGMA Q8 - Q11). The non-isotropic shrinkage behavior of semi-crystalline polymers (POM, PA46, PEEK) is balanced by involute profile modification of the mold cavity electrodes and radial shrinkage compensation. The cavities are machined into hardened stainless steel (DIN 1.2083 ESR) using micron-precision Wire EDM and Jig Grinding machines.

Smart injection with in-mold pressure sensors.
September 26 195 Views

Smart injection with in-mold pressure sensors.

In-mold pressure and temperature sensors are piezoelectric and infrared (IR) based Industry 4.0 devices that measure the dynamic rheological state of the molten polymer in mold cavities in milliseconds. Instead of relying on the hydraulic pressure of the injection molding machine, these systems read the actual plastic pressure directly within the cavity; they dynamically manage the velocity-to-pressure switchover using the Decoupled III methodology. This technology compensates for inter-batch viscosity fluctuations, preventing flash, short shots, and shrinkage marks at the source, and integrates with part sorting robots to ensure 100% part quality classification.

2K Injection Molding and Design Principles (Two-Component)
September 26 208 Views

2K Injection Molding and Design Principles (Two-Component)

Two-component (2K / Two-Color / Multi-Component) injection molding is the process of joining two different polymers (typically a rigid thermoplastic skeleton with a soft TPE/TPU elastomer, or two different colors) at the molecular level in a single cycle using an injection molding machine, rotary table, or transfer robot. Eliminating gluing, screwing, or secondary assembly labor, 2K technology is used in automotive interior trims, power tool housings, and industrial enclosures with integrated sealing gaskets. A successful 2K process depends on the chemical compatibility table based on the surface energies of the polymers, optimized shrinkage compensation, and micron-precise locking systems in male/female cavities.

Medical LSR (Liquid Silicone) molding technology
September 26 152 Views

Medical LSR (Liquid Silicone) molding technology

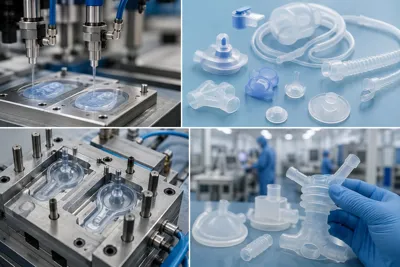
In the medical sector, LSR (Liquid Silicone Rubber) molding is an advanced manufacturing method achieved by precisely dosing two-component (A and B) low-viscosity platinum-cured silicone at a 1:1 volumetric ratio, mixing it in a static mixer, and injecting it into hot mold cavities (170°C - 200°C). This process, conducted under ISO 13485 quality management system and ISO Class 7/8 cleanroom infrastructure, ensures full compliance with USP Class VI and ISO 10993 biocompatibility standards, zero flashless precision, and micron-level micro-injection capability. Cold-deck closed valve systems minimize raw material waste.

Production of high-strength sealing elements.
July 26 406 Views

Production of high-strength sealing elements.

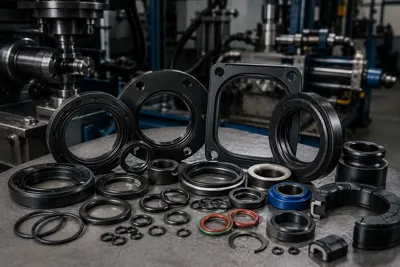
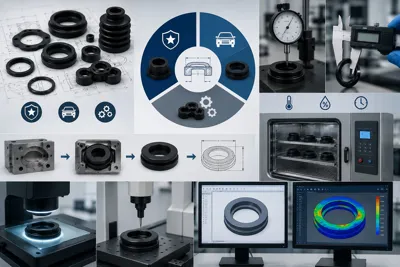
The production of sealing elements for the machinery industry aims to prevent fluid loss in hydraulic and pneumatic systems, withstand high system pressures (350 to 700 bar), and minimize dynamic wear. NBR, HNBR, FKM (Viton), and Polyurethane (PU) elastomeric raw materials are used in the manufacturing processes. Production verification is carried out according to DIN 3760 (rotary shaft seals) and TS ISO 3601-1 (o-rings) standards, while the elastic recovery capabilities of the parts are guaranteed by ASTM D395 permanent deformation (compression set) criteria.

Indentation and deformation in plastic mold design.
July 26 347 Views

Indentation and deformation in plastic mold design.

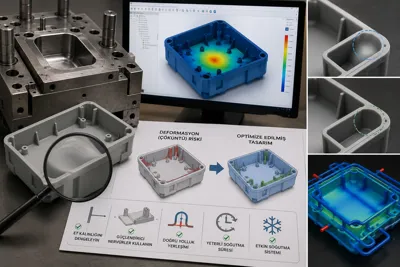
Sink marks and dimensional warpage in plastic mold design result from volumetric shrinkage differences in areas with high wall thickness during the cooling phase of the molten polymer. To prevent these aesthetic and geometric defects, the base wall thickness should be kept homogeneous during the design phase, and the base thickness of the structural support ribs should be dimensioned so that it does not exceed 50% - 60% of the base wall thickness. Positioning the mold cooling channels at equal distances from the male and female cores and optimizing the holding pressure profile with Moldflow thermal simulations guarantees dimensional stability according to ISO 20457 standards.

Prototype molding and mass production cost advantages
July 26 379 Views

Prototype molding and mass production cost advantages

Soft tooling is a pre-series manufacturing method that enables the rapid and low-cost production of 50 to 5,000 actual raw material parts before resorting to costly mass production molds (hard tooling). It is typically manufactured using easily machinable aluminum alloys (Alumec 89, 7075 T6) or pre-hardened mild steels (1.2311). Thanks to soft tooling, assembly, strength, DFM verification, and PPAP sample testing of the final part can be performed under real injection molding conditions, minimizing the risk of high revision costs associated with mass production.

Wear protection in rubber molds and extending mold life.
July 26 322 Views

Wear protection in rubber molds and extending mold life.

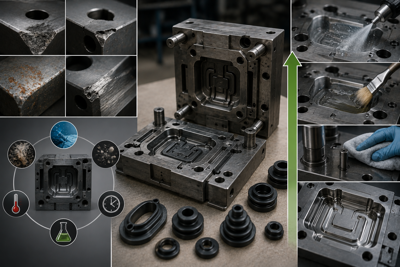
Wear in rubber molds is a combination of chemical corrosion caused by acidic gases released by sulfur and peroxide-based agents in the raw material during vulcanization (160°C - 200°C) and physical abrasion (friction) caused by carbon black/mineral fillers. To extend mold life, DIN 1.2344 hot work tool steels with a hardness of at least 48-52 HRC are preferred in the cavities, and CrN (Chromium Nitride) or PVD coatings are applied to the steel surfaces to increase wear resistance. As part of periodic mold maintenance, mold release residues and polymer gas deposits are removed using chemical solvents in ultrasonic cleaning units that do not damage the steel geometry.

Engineering plastics (PA6, POM, PC) and their properties.
July 26 336 Views

Engineering plastics (PA6, POM, PC) and their properties.

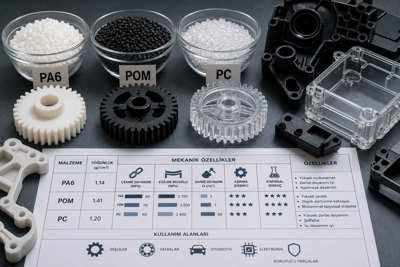
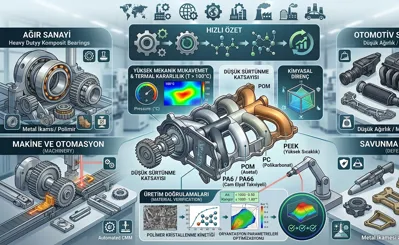
Engineering plastics (PA6, POM, PC) are technical polymers that replace metal components in industrial manufacturing by offering high tensile strength (60 MPa), modulus of elasticity, dimensional stability, and thermal wear resistance. Polyamide 6 (PA6) exhibits high impact damping and mechanical toughness, while polyoxymethylene (POM/acetal) is used in precision mechanical gears due to its low coefficient of friction (0.15 - 0.25) and near-zero moisture absorption. Polycarbonate (PC), on the other hand, offers optimized engineering solutions for molding structurally transparent components with its high light transmittance (89%) and extreme impact resistance.

Strategies for Reducing Mold Costs
July 26 320 Views

Strategies for Reducing Mold Costs

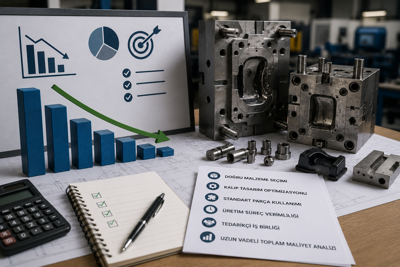
Strategies for reducing mold costs include eliminating undercuts through DFM (Design for Manufacturing) analyses during product development (R&D), optimizing part wall thicknesses, and simplifying core mechanisms. Selecting cavitation (number of cavities) and steel grades according to SPI standards (e.g., 1.2311 vs. 1.2344) based on annual part projections optimizes the initial mold investment cost (CAPEX) by 30% to 50%. The use of modular mold holder systems and standard mold elements permanently reduces CNC machining times and per-part depreciation costs.

Rubber injection and compression molding
July 26 342 Views

Rubber injection and compression molding

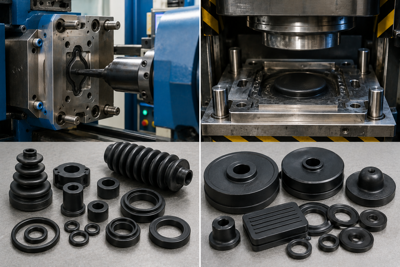
Rubber injection molding and compression molding are two fundamental industrial methods that manage the vulcanization processes of elastomeric raw materials. Rubber injection molding is based on the principle of plasticizing the raw material in a screw-barrel system at a temperature of 70°C - 90°C and then pressing it under high pressure into closed and hot (170°C - 200°C) mold cavities. Compression molding, on the other hand, involves placing pre-shaped raw material (preform) directly into an open mold and shaping it with hydraulic press pressure. While the injection method is ideal for high-volume, precisely toleranced, and complex geometric OEM parts; the compression method provides high cost/performance for large-sized components and low-budget prototype manufacturing.

Burr problems in plastic injection molding and solutions.
July 26 354 Views

Burr problems in plastic injection molding and solutions.

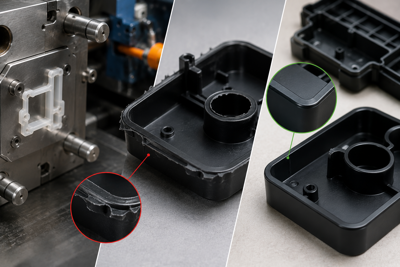
In plastic injection molding, flash is a dimensional and aesthetic manufacturing defect caused by molten polymer leaking out of mold parting lines, core surfaces, or ejector pin cavities under high injection pressure (>1000 bar). This problem stems from insufficient clamping force, excessive injection speed, mechanical crushing or abrasion of mold kissing surfaces, or polymer melt temperatures that excessively reduce viscosity. Solutions include optimizing compression ratios through Moldflow analysis and revising mold steels with micron-precision laser welding or CNC grinding.

EPDM, NBR, and Silicone: Which rubber raw material should be chosen?
July 26 389 Views

EPDM, NBR, and Silicone: Which rubber raw material should be chosen?

The selection of rubber raw materials is based on the continuous operating temperature to which the final elastomeric part will be exposed, the chemical fluids it will come into contact with (oil, fuel, solvent), and the environmental factors it will be exposed to (ozone, UV, weather conditions). NBR (Nitrile) offers superior mineral oil and fuel resistance between -30°C and +110°C, while EPDM provides excellent ozone, UV, and steam resistance in the range of -40°C to +140°C. Silicone (VMQ), on the other hand, demonstrates full compliance with food and medical standards (FDA) with its physiological harmlessness in the extreme thermal spectrum of -60°C to +220°C.

How is steel selected for plastic injection molds?
July 26 390 Views

How is steel selected for plastic injection molds?

Steel selection for plastic injection molds depends on the abrasiveness of the polymer to be molded, the annual production volume (SPI classes), and the expected surface finish of the part. For abrasive glass fiber reinforced (GF) polymers, vacuum-hardened DIN 1.2344 hot work steel with a hardness of 48-52 HRC is suitable; for transparent or corrosive PVC/fluoropolymer components, stainless DIN 1.2083 steel containing a minimum of 13% chromium is recommended; and for standard body parts, pre-hardened DIN 1.2738 (P20+Ni) steel offers optimized metallurgical solutions.

Rubber tolerances and TS ISO 3302-1 standard guide.
June 26 607 Views

Rubber tolerances and TS ISO 3302-1 standard guide.

In industrial rubber products, dimensional and geometric tolerances are determined according to the TS ISO 3302-1 standard due to the high shrinkage (1.5% - 4%) and elasticity characteristics of elastomers. This international standard classifies molded parts into three basic classes based on their dimensional accuracy: M1 (Precision/Defense), M2 (High Quality/Automotive), and M3 (Commercial/General Machinery). Measurements are verified using optical and digital measuring instruments in climate-controlled laboratory environments at a temperature of 23°C +/- 2°C and 50% relative humidity, at least 16 hours after the part has completed its vulcanization reaction and thermal stabilization.

Technical plastic products and industrial applications.
June 26 373 Views

Technical plastic products and industrial applications.

Technical plastic products are components manufactured using engineering plastics (PA6, PA66, POM, PC, PEEK) that, unlike conventional polymers, offer high mechanical strength, thermal stability up to 100°C, chemical resistance, and a low coefficient of friction. They are frequently preferred in metal replacement projects in heavy industry, machinery, automotive, and defense sectors. Production validations are carried out according to ISO 20457 geometric tolerance standards by optimizing the crystallization kinetics and orientation parameters of the polymers.

Contract manufacturing of plastic parts and mold integration.
June 26 358 Views

Contract manufacturing of plastic parts and mold integration.

Contract manufacturing of plastic parts is the process of integrating existing injection molds, owned by the customer, into the manufacturer's machine park for mass production. During the mold integration phase, the mold's mounting plates, ejector group, runner dimensions, and cooling nipple inlets are adapted to the technical specifications of the injection molding machine (50-1200 tons). Raw material drying operations (using dew-point honeycomb dryers), melting temperature control, and part quality are monitored according to ISO 9001 standards to optimize unit costs per part.

Mass production molds and high-volume manufacturing solutions.
June 26 442 Views

Mass production molds and high-volume manufacturing solutions.

High-volume series production mold manufacturing is an engineering discipline applied to minimize cycle times and increase line efficiency (OEE) to over 85%. In high-volume manufacturing lines, powder metallurgical steels (Bohler M390, Elmax, etc.) with a hardness of 52-54 HRC according to the SPI Class 101 standard and corrosion-resistant DIN 1.2083 alloys are used. In multi-cavity molds, hot runner systems and conformal cooling channels that follow the part geometry in 3D are integrated for a balanced polymer distribution.

Guide to choosing a plastic injection mold manufacturer.
June 26 502 Views

Guide to choosing a plastic injection mold manufacturer.

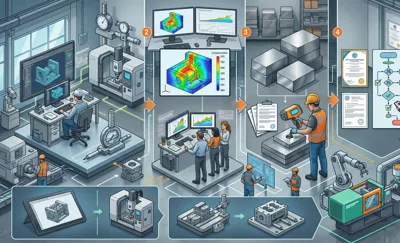
Choosing a plastic injection mold manufacturer involves verifying the supplier's CAD/CAM infrastructure, CNC precision limits (in the micron range), DFM (Design for Manufacturability) competence, and compliance with ISO 9001/IATF 16949 quality management systems. A reliable mold manufacturer should document steel supply with spectrometer analysis certificates (DIN 1.2344, 1.2738, etc.), provide Moldflow flow simulation outputs, and guarantee mold life according to international SPI (Society of Plastics Industry) standards. Integrating design, manufacturing, and mass production injection lines under a single roof reduces project operational risks by 40%.

Defense industry rubber part manufacturing, Military standards.
June 26 454 Views

Defense industry rubber part manufacturing, Military standards.

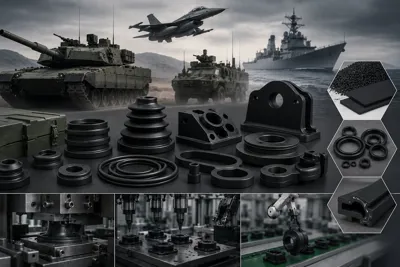
Defense industry rubber component manufacturing is the process of producing elastomer components that withstand extreme environmental conditions in accordance with MIL-STD, MIL-SPEC, and ASTM standards. Sealing elements and damping pads produced for military land, sea, and air platforms are molded with traceable raw materials compliant with the NATO codification system. Mechanical testing of FKM (Viton), Fluorosilicone (FVMQ), and Nitrile (NBR) based components produced for hydraulic systems, fuel tanks, and avionics protection units is verified and certified on a part-by-part basis in accredited laboratory environments.

Custom-designed plastic molds and mass production solutions.
June 26 352 Views

Custom-designed plastic molds and mass production solutions.

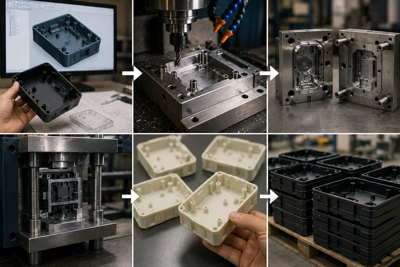
Custom plastic mold manufacturing is the process of transforming conceptual product designs (3D CAD) into functional steel mold cavities using Moldflow plastic flow and thermal cooling simulations. In the mass production phase, servo-hydraulic plastic injection molding machines with clamping forces ranging from 50 to 1200 tons are used, depending on the part geometry. Production processes are optimized according to the crystallization and shrinkage parameters of industrial polymers such as PP, ABS, PC, POM, and PA66, ensuring sustainable part quality according to ISO 20457 dimensional tolerance standards.

Automotive rubber and plastic parts manufacturing and OEM solutions.
June 26 495 Views

Automotive rubber and plastic parts manufacturing and OEM solutions.

In the automotive sub-industry, the production of rubber and plastic parts is carried out according to IATF 16949 Quality Management System standards. Active production processes include high-temperature and oil-resistant ACM, AEM, and FKM (Viton) compounds for engine seals, and natural rubber (NR) and EPDM formulations for dynamic damping in suspension lines. Dimensional verifications are performed using 3D CMM devices within the scope of PPAP (Production Part Approval Process) processes and are guaranteed to meet TS ISO 3302-1 M1/M2 accuracy classes.

Plastic injection mold prices and cost guide.
June 26 573 Views

Plastic injection mold prices and cost guide.

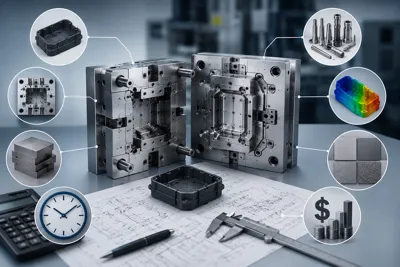
Plastic injection mold prices are determined by part dimensions (mm), cavitation (number of cavities), mechanical core/hydraulic system requirements, and the metallurgical properties of the selected steel alloy (1.2344, 1.2738, 1.2311). Hot runner integration reduces runner waste to zero while increasing the initial mold investment cost by 15% to 30%. Mold life classes are classified as Class 101 (1 million+ cycles) and Class 103 (less than 100,000 cycles) according to SPI (Society of Plastics Industry) standards, and pricing is directly optimized according to these engineering classes.

Rubber mold manufacturing and industrial production solutions.
June 26 530 Views

Rubber mold manufacturing and industrial production solutions.

Rubber mold manufacturing is the process of shaping elastomer raw materials through vulcanization reactions under high temperatures (160°C - 200°C) and pressures (50 - 250 bar). Compression, transfer, and injection molding methods are used in industrial production lines. Production tolerances are determined according to the TS ISO 3302-1 standard M1, M2, and M3 classes, while the storage and shelf life criteria of the final elastomeric components are subject to the DIN 7716 standard. High-precision sealing and damping elements are produced for the automotive, defense, and machinery industries using NBR, EPDM, FKM (Viton), and silicone raw materials.

Call Us Call Us

Useful Content Selected for You

View All →
Prototype molding and mass production cost advantages
379 Reads

Prototype molding and mass production cost advantages

Soft tooling is a pre-series manufacturing method that enables the rapid and low...

Production of high-strength sealing elements.
406 Reads

Production of high-strength sealing elements.

The production of sealing elements for the machinery industry aims to prevent fl...

Engineering plastics (PA6, POM, PC) and their properties.
336 Reads

Engineering plastics (PA6, POM, PC) and their properties.

Engineering plastics (PA6, POM, PC) are technical polymers that replace metal co...

Custom-designed plastic molds and mass production solutions.
352 Reads

Custom-designed plastic molds and mass production solutions.

Custom plastic mold manufacturing is the process of transforming conceptual prod...

Contract manufacturing of plastic parts and mold integration.
358 Reads

Contract manufacturing of plastic parts and mold integration.

Contract manufacturing of plastic parts is the process of integrating existing i...